Picture a typical aerospace industry floor mid-shift: a nesting file loaded, titanium stock staged at the machine, and a production schedule that doesn't have room for a machine that can't keep pace. That's the real starting point for sizing a fiber laser for aerospace industry, not a spec sheet in isolation. Aerospace Industry work is suppliers working to tighter edge-quality and traceability requirements, often on titanium and aluminum alloys, where a laser's repeatable, narrow heat-affected zone helps hold certification-relevant tolerances, and that shapes which fiber laser configuration actually makes sense more than any single spec on a data sheet.

SF Series Small Precision Fiber Laser Cutting Machine -- one of the configurations covered below for aerospace industry.
This page covers what actually differs for aerospace industry: typical material and thickness, running-cost drivers specific to this work, how the job looks from the operator's chair versus the engineer's or the buyer's side of the table, and which PCL Group configuration fits which shop size.
Aerospace Industry: What Each Power Tier Actually Cuts
Rather than a generic thickness chart, here's what a aerospace industry shop typically runs at each power tier, alongside the published titanium thickness capacity for reference:
| Power | Machine | Typical Aerospace Industry Job | Titanium Capacity |
|---|---|---|---|
| 500W | SF Series Small Precision Fiber Laser Cutting Machine | thin titanium or aluminum alloy prototype brackets and test coupons | send your job specs -- we'll confirm |
| 750W | SF Series Small Precision Fiber Laser Cutting Machine | small aerospace brackets and clips in thin-gauge titanium or aluminum alloy | send your job specs -- we'll confirm |
| 1000W | DF Series Fiber Laser Cutting Machine (DF2040) | production runs of thin-to-medium aerospace brackets where certification-relevant edge quality matters | send your job specs -- we'll confirm |
| 1500W | DF Series Fiber Laser Cutting Machine (DF2040) | medium-gauge structural aerospace brackets and panel components | send your job specs -- we'll confirm |
| 2000W | DF Series Fiber Laser Cutting Machine (DF2040) | heavier aerospace-adjacent structural parts, though most aerospace sheet work stays well under this | send your job specs -- we'll confirm |
| 3000W | DF Series Fiber Laser Cutting Machine (DF2040) | an uncommon tier for aerospace sheet specifically -- usually relevant only in a mixed job shop that also cuts thicker material | send your job specs -- we'll confirm |
Job descriptions reflect what we most commonly see ordered at each tier for this industry, not a hard ceiling -- a heavier or lighter job mix shifts the right tier up or down.
Titanium Thickness in Aerospace Industry: What's Typical
We don't publish a single blanket thickness chart for titanium across every power tier -- send your typical aerospace industry part thickness and we'll confirm the exact configuration rather than guess from an average.
For the complete titanium power-and-thickness breakdown (500W to 30,000W, every tier we build), see our dedicated fiber laser cutting machine for titanium guide -- this page focuses on what's specific to aerospace industry rather than repeating that full chart.
Running Cost in Aerospace Industry: Power, Labor, and Fume Extraction
Power Draw & Electricity Cost
Idle time still costs money in aerospace industry: a machine sitting between jobs with its chiller and cabinet electronics running draws power without cutting anything. Shops that batch nesting to keep the head cutting rather than waiting on operator load/unload see a real difference in electricity cost per finished part, independent of which power tier they bought.
Labor
We won't tell a aerospace industry shop exactly how many people a given configuration needs, since that depends on your existing workflow, but we will say plainly where labor gets absorbed: setup and programming time on a new job, loading/unloading between cuts, and any secondary finishing the cut edge still needs. Ask us to walk through all three for your specific parts before you size a crew around a new machine.
Three Perspectives on Cutting Titanium for Aerospace Industry
A machine purchase for aerospace industry gets evaluated differently depending on who in the shop is looking at it -- here's the same decision from three real vantage points:
changeover time between jobs matters as much as cutting speed on a shift that runs a lot of different aerospace industry parts -- swapping a nesting file and reloading sheet stock should take minutes, not require reprogramming cutting parameters from scratch.
heat-affected zone width and edge microstructure are real engineering concerns on aerospace industry parts that get welded, heat-treated, or stressed after cutting -- a narrower HAZ from a well-tuned fiber laser cut gives more margin in downstream processing than a wider one from an under-optimized setup.
financing and total landed cost (freight, duties, installation) matter as much to a aerospace industry buyer's decision as the machine price itself -- we treat that as part of the quote conversation, not a follow-up surprise after the fact.
None of these views is more "correct" than the others -- a configuration that only satisfies one of them (say, the lowest sticker price with none of the operator's or engineer's concerns addressed) tends to become an expensive mistake within the first year of aerospace industry production.
Real Jobs, and Mistakes Worth Avoiding
A Typical Job
A common real-world case in aerospace industry: a medical device manufacturer cutting titanium implant blanks that will go through additional finishing and inspection.
A Mistake Worth Avoiding
For aerospace industry work specifically: titanium fires can occur if assist gas coverage is inadequate at the cut zone -- this is a real safety consideration, not just a quality one, and it's part of why titanium cutting parameters shouldn't be improvised from steel settings.
Signs a Fiber Laser Actually Fits Your Aerospace Industry Shop
Not every aerospace industry shop needs the same configuration -- these are the real signals we listen for on an inquiry call:
- Your parts carry certification or traceability requirements on edge quality.
- You cut titanium or aluminum alloy and can't tolerate an inconsistent heat-affected zone.
- Rejects for tolerance, not lateness, are your most common quality complaint.
Configuration by Shop Size: Aerospace Industry
The same underlying question comes up regardless of shop size: which configuration actually matches how a aerospace industry shop will use it, day to day. Three common starting points:
Job-Shop / Entry Configuration
A shop cutting aerospace industry parts as one line among several jobs, rather than as dedicated production, is usually better served starting with an SF-class machine -- enough precision and power for typical titanium gauge without paying for worktable size or automation a low-volume line won't use.
Production / Multi-Shift Configuration
Once aerospace industry work is running across multiple shifts with real downtime cost, the LF Series' heavier-duty bed and higher power ceiling earn their keep over a lighter machine sized for occasional use.
High-Precision Configuration
Where aerospace industry parts get rejected for tolerance or edge-quality reasons more than for being late, our SF Series' tighter repositioning accuracy is built for exactly that trade-off against raw throughput.
How to Choose a Fiber Laser Cutting Machine for Aerospace Industry
Buyers in aerospace industry tend to focus on power first -- power matters, but these five checks catch most of the expensive mistakes we see on this specific type of order:
- Size power to your thickest regular aerospace industry part, not your thinnest -- the most common expensive mistake we see.
- Confirm assist gas delivery for titanium at the pressure your typical thickness needs.
- Match worktable size to your actual stock, with nesting room rather than a bed sized to the exact sheet.
- Ask for a software demo, not just a spec sheet -- your operators will live in the nesting/cutting interface daily.
- Check regional warranty and spare-parts support before ordering, especially for source-specific consumables.
Fiber Laser vs. Plasma vs. Waterjet for Aerospace Industry
All three processes show up somewhere in aerospace industry, and the honest comparison depends on thickness and finish requirements more than any single "best" answer:
| Factor | Fiber Laser | Plasma | Waterjet |
|---|---|---|---|
| Edge quality | Best of the three -- near weld-ready, minimal secondary finishing | Rougher, usually needs grinding before welding | Very clean, but slower and adds moisture to the cut zone |
| Typical thickness sweet spot | Thin to medium gauge, extending further with higher power | Thick plate at the lowest cost per cut | Any thickness, but throughput drops as it increases |
| Heat-affected zone | Narrow | Wider -- can matter for parts that get welded or heat-treated after | None -- a cold cutting process |
| Running cost driver | Assist gas + electricity, scales with speed | Consumable electrodes/nozzles, generally cheaper per cut on thick plate | Abrasive garnet consumption, generally the most expensive per cut |
For titanium specifically at the thickness most aerospace industry shops run, fiber laser wins on speed and edge quality; plasma remains a reasonable choice purely on cost for very thick plate, and waterjet is worth considering only where zero heat input is a hard requirement.
Fiber Laser vs. What Most Aerospace Industry Shops Ran Before
Shops moving aerospace industry work onto a fiber laser are usually replacing plasma, oxy-fuel, or a manual cutting process, and the switch is rarely just about speed -- the edge quality difference is what actually changes downstream work in aerospace industry, since a cleaner cut on titanium means less grinding or deburring before the part moves to its next step. See the full process comparison table above for the general tradeoffs across fiber laser, plasma, and waterjet.
To be equally honest about the other direction: fiber laser is not automatically the right call for every aerospace industry job. Very thick plate at the extreme end of a job mix, parts that genuinely can't tolerate any heat input, or volumes too low to justify any dedicated cutting equipment are all cases where a different process -- or subcontracting the occasional outlier job -- can beat owning a machine sized for your rare, not your typical, part.
Beyond Titanium: Other Materials Aerospace Industry Shops Run
Aerospace Industry work rarely means a single material all day -- shops in this space commonly also run Aluminum and Aluminum Alloy, each with its own assist gas and cutting-parameter requirements. If your job mix spans more than one of these, size your machine and gas delivery to the hardest material in the mix, not the easiest.
Automation and Downstream Processes in Aerospace Industry
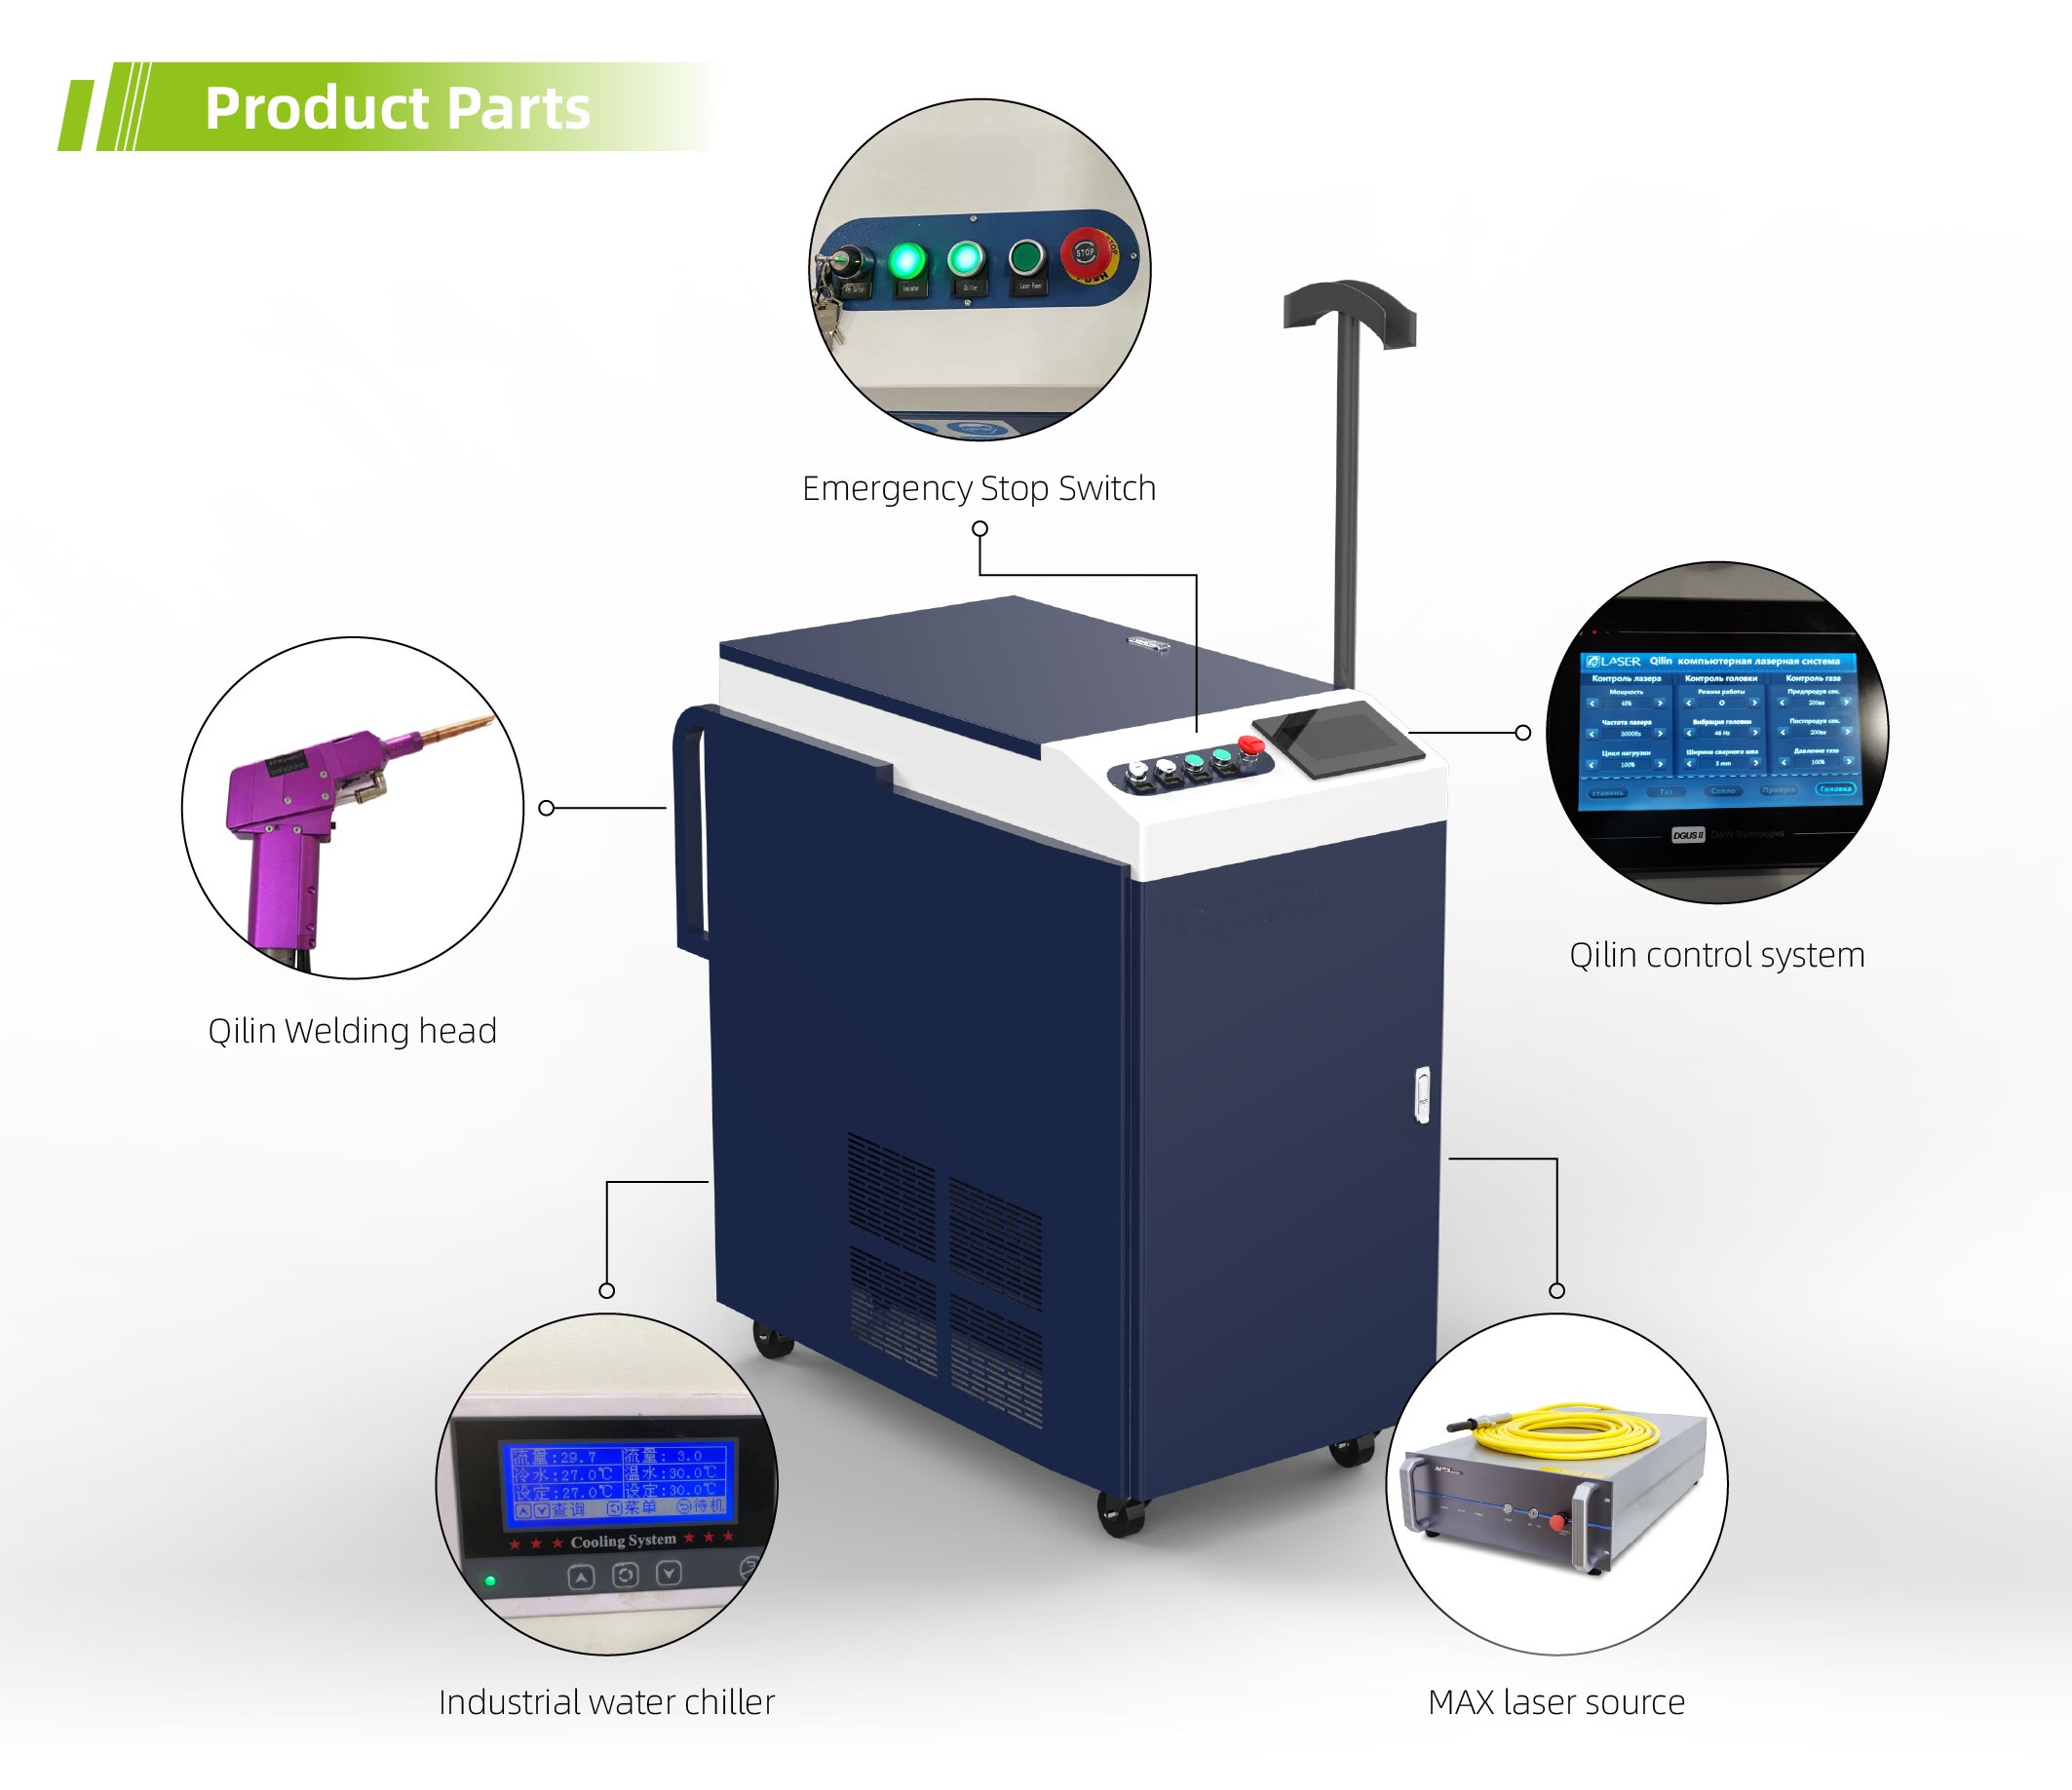
Cutting is one step in a longer aerospace industry workflow, not the whole job. Many shops in this space also run a handheld fiber laser welding machine downstream of the laser -- narrow heat-affected zone keeps warping and discoloration to a minimum on thin sheet -- which is worth planning for when you're laying out floor space and staffing around a new cutting machine, not treating as a separate purchase decision made later.
The practical link for aerospace industry: a cleaner, more consistent titanium cut edge coming off the laser directly reduces the fit-up and rework time on whatever comes next on a aerospace industry floor, whether that's welding, bending, or assembly -- part of why the cut-quality numbers earlier on this page matter beyond the cutting step itself.
Total Cost of Ownership
The purchase price is only the first number that matters when budgeting fiber laser cutting for aerospace industry. Over a typical 3-5 year service life, argon consumption, electricity, and wear parts (nozzles, protective lenses, and eventually the cutting head) add up to a running cost that often rivals the purchase price itself -- and on titanium specifically, that cost scales with how close to the machine's rated thickness ceiling you run day to day.
Nesting efficiency matters more the higher titanium stock costs per sheet -- software that minimizes offcuts pays for itself faster on higher-value material than on inexpensive, scrap-tolerant metal, which is worth factoring into the aerospace industry cost picture alongside the running-cost drivers above.
Software, Support, and Export
Operators programming aerospace industry jobs spend more working time in the control software's nesting and cutting-parameter interface than at the laser source itself -- our machines run nesting software built for shop-floor use, which shortens the learning curve on new titanium jobs. Installation guidance and operator training are included with every order.
PCL Group manufactures and exports this equipment directly rather than reselling another factory's design, and ships to aerospace industry buyers worldwide. Lead time depends on configuration and current factory schedule -- each machine is built and tested against your specific requirements rather than pulled off a shelf -- and we keep spare parts (nozzles, lenses, source-specific components) in stock rather than sourcing them after a machine cutting titanium is already running.
Common Concerns Before Ordering
Buyers in aerospace industry sometimes worry that after-sales support disappears once a machine ships from overseas. Our engineering team stays reachable directly for technical questions well after installation, and we keep spare parts stocked for titanium-relevant consumables because we know that gap is where overseas purchases most often go wrong for other buyers.
After an initial inquiry about aerospace industry work, expect a short back-and-forth to confirm your material, thickness, and monthly volume, followed by a written quote for a specific configuration -- not a generic price list. Production begins once terms are confirmed, with lead time depending on configuration and current factory schedule.
Frequently Asked Questions
What's the best fiber laser cutting machine for aerospace industry?
It depends on your typical titanium thickness and volume -- for most aerospace industry shops we start the conversation around the SF Series Small Precision Fiber Laser Cutting Machine, then adjust power and worktable size from there.
How much does running cost matter for aerospace industry compared to the machine price?
For aerospace industry work, more than most buyers expect -- assist gas (argon for titanium), electricity, and downstream labor (grinding, deburring) all add up over the machine's service life on a aerospace industry floor. See the running-cost section above for specifics.
Do I need special fume extraction for aerospace industry?
For aerospace industry specifically, it depends on the material in your job mix, not the industry name -- we size fume extraction to whichever material you run needs the most, and will tell aerospace industry buyers honestly if that means an upgrade from what they currently run.
How many operators does a fiber laser cutting machine need for aerospace industry work?
We don't publish a fixed staffing number for aerospace industry because it depends on your loading, unloading, and finishing workflow -- ask us to walk through your specific aerospace industry process and we'll give you a realistic answer, not a generic one.
Can one machine handle the full range of parts a aerospace industry shop typically runs?
For most aerospace industry shops, often yes within one material's thickness range, but a job mix that spans several metals or a wide thickness range may point to a different configuration than a single-material aerospace industry operation -- send us your actual part mix and we'll confirm.
What's the lead time for a fiber laser cutting machine ordered for aerospace industry?
For a aerospace industry order, lead time depends on configuration and current factory schedule, since each machine is built and tested against your specific requirements rather than shipped off a shelf -- we'll give you a specific timeline as part of your aerospace industry quote.
Should a small aerospace industry shop start with a smaller machine and upgrade later?
For a smaller aerospace industry operation, often yes -- if your titanium volume today doesn't justify a full production-scale machine, an entry-tier configuration sized to your current thickest aerospace industry job is usually the safer financial choice over stretching the budget for headroom you may not use for another year or two.
Do you offer installation and operator training for aerospace industry customers?
Yes -- for every aerospace industry order, installation guidance and operator training on the nesting and cutting-parameter software are included regardless of which configuration you choose.
What assist gas does titanium cutting use in aerospace industry applications?
In aerospace industry work, argon is the standard choice for titanium -- titanium is chemically reactive at cutting temperatures and will absorb nitrogen or oxygen from a non-inert atmosphere, which is why argon (or high-purity nitrogen for non-critical parts) is used to protect the microstructure at the cut edge.
What's the difference between a 1000W and a 3000W fiber laser for aerospace industry?
For aerospace industry work, the difference is mainly thickness ceiling and cutting speed on titanium -- see the power-tier table above for what we typically see ordered at each tier for aerospace industry specifically, rather than assuming a generic doubling of capability per tier.
Do aerospace industry shops usually need automation beyond the cutting machine itself?
For aerospace industry specifically, often yes, downstream of the cut rather than at the laser itself -- see the automation and downstream processes section above for what we commonly see paired with fiber laser cutting in this industry.


